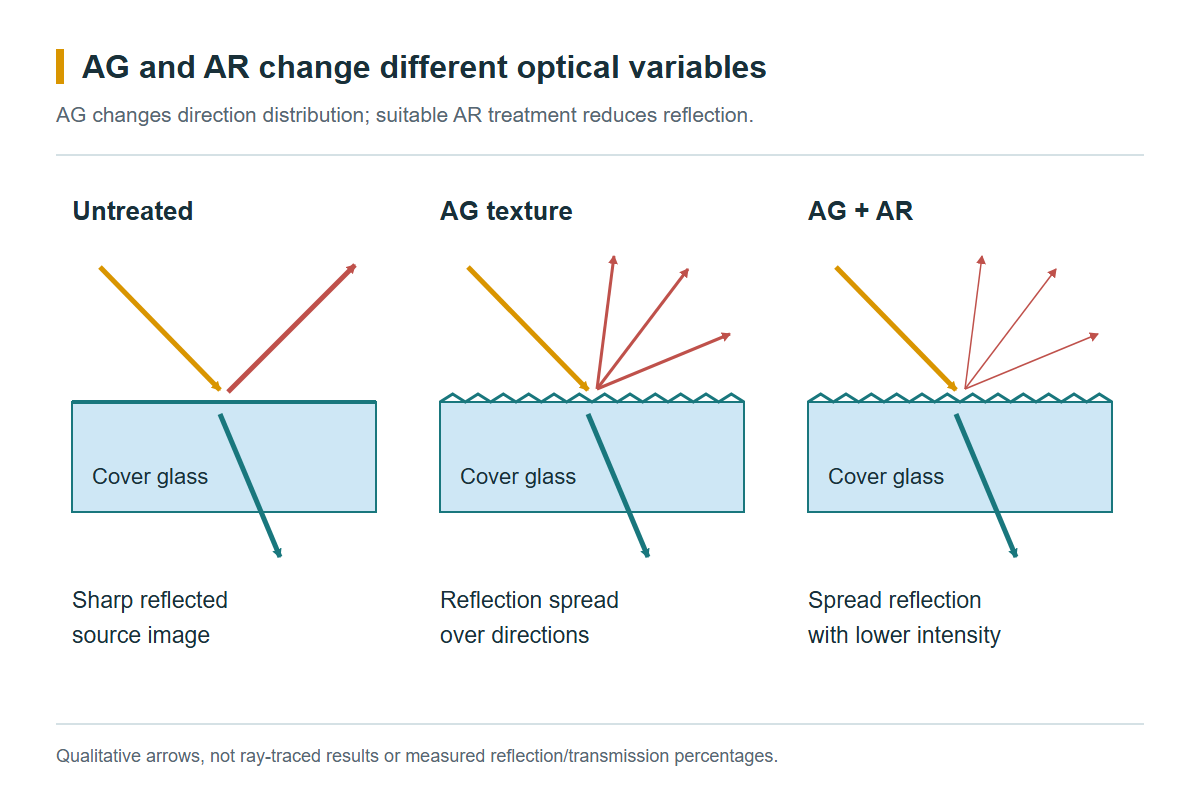
A display can have two reflection problems at once. A ceiling light may appear as a sharp, distracting image, while reflected ambient light also makes dark screen content look lighter. Anti-glare (AG) and anti-reflective (AR) treatments address different parts of that problem, which is why they are sometimes combined on display cover glass.
AG changes how reflected light is distributed. AR reduces reflected light within its designed optical conditions. A useful combination balances the two without sacrificing more image clarity than the application can tolerate.
AG Blurs a Reflection; AR Reduces Its Intensity
An AG surface uses texture to spread reflection across a range of directions. The outline of a reflected lamp becomes less distinct, but the texture can also scatter display light travelling outwards. That is the source of an important trade-off: reducing a sharp reflection is not the same as keeping fine screen details unchanged.
AR treatment acts through the optical behaviour of the treated interface. Thin-film interference is one common method of reducing reflectance; the coating is designed around its substrate, wavelength range and angles of incidence. Edmund Optics explains this distinction in its anti-reflection coating guide.
The practical objective is not to make the surface as matt as possible. It is to make the displayed information easier to read in its expected lighting.
Why AG Alone Can Leave a Pale-Looking Screen
Spreading a reflection can turn a concentrated bright image into a broader veil over the screen. Dark areas may then look pale under ambient illumination. Adding suitable AR treatment can reduce the reflected contribution while retaining the AG surface’s less distinct reflections.
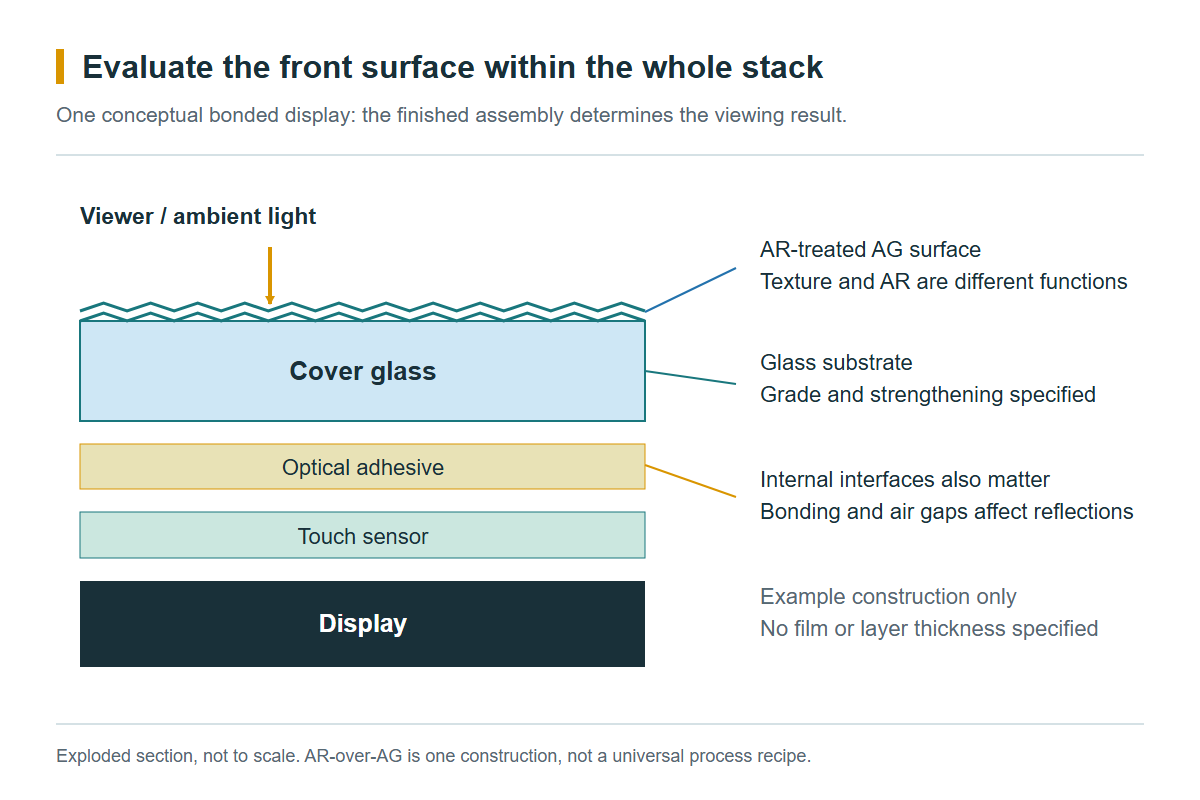
This is not only a theoretical pairing. Nippon Electric Glass describes an AG+AR display-cover product that places an AR coating over AG treatment, and shows a comparison between untreated, AG-only and AG+AR surfaces. Its published optical figures are examples for that product, not recommended targets for all industrial displays.
An AR layer over an AG surface is one possible construction. It is not a universal recipe: texture, substrate, strengthening, coating process and any fingerprint treatment have to be compatible.
The Best Choice Is Not Always AG+AR
| Viewing requirement | Candidate to evaluate | Main compromise to check |
|---|---|---|
| Fine text with controlled indoor lighting | Clear glass with AR | Remaining distinct reflections and viewing-angle colour |
| Strong, sharply defined reflected lamps | AG, with AR if needed | Haze, sparkle and fine-detail visibility |
| Mixed bright ambient light and distracting source images | Balanced AG+AR | Whether the combination improves the actual display |
| A low-cost, protected control interface | Clear glass or restrained AG | Whether extra treatment changes usability enough to justify cost |
These are starting points for sample evaluation, not fixed product rules. A high-resolution inspection monitor and a large-symbol machine control panel do not need the same surface.
Haze, Gloss and Sparkle Answer Different Questions
Haze describes transmitted-light scattering under a defined measurement method. Gloss describes the strength of a directed surface reflection at a stated geometry. Sparkle concerns spatial brightness variations seen with a pixelated display through the surface.
A surface with low gloss is therefore not automatically a good high-resolution cover. Nor does a low reflectance result prove that small fonts remain sharp. NEG treats low sparkle as a separate design concern in its AG coating information.
For an optical specification, identify the haze and gloss methods, the reflectance wavelength range and angle, and the display used for sparkle evaluation. Two figures measured under different conditions may not be directly comparable. NEG’s separate AR information also illustrates that the target wavelength range can be customised.
Evaluate the Cover on the Display, Not Only on the Bench
A loose glass sample is useful for checking texture and coating appearance. It cannot reproduce the full optical assembly. Internal interfaces, a bonding layer or an air gap can change the reflections the viewer sees.
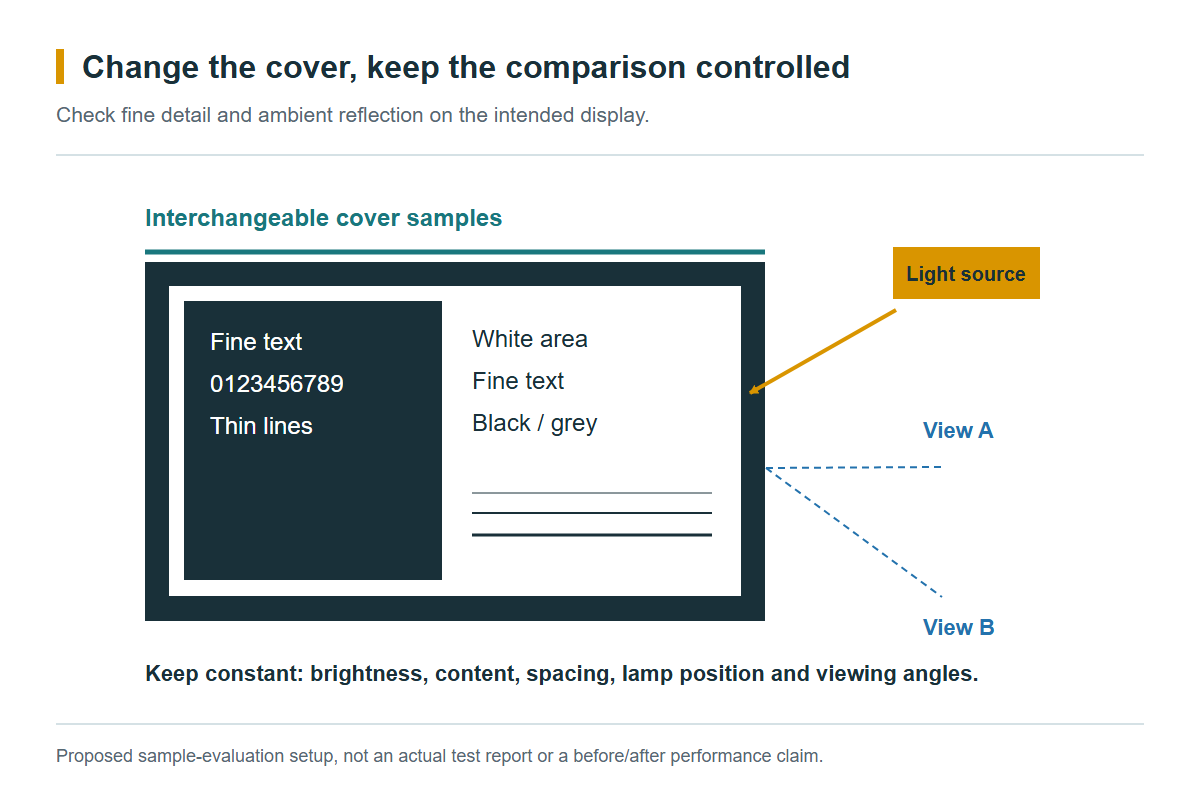
For a side-by-side trial, keep the display content, brightness, cover-to-display spacing, lamp position and viewing angle unchanged. Include black areas, white backgrounds, fine lines and the smallest text the operator must read. Change only the cover sample first; otherwise it becomes difficult to identify what caused the improvement.
After the visual trial, assess the selected coating against the actual cleaning chemicals, wipe cycles and environment. A clean new sample does not demonstrate performance after service wear.
AG and AR are used together because reflection direction and reflected intensity are different design variables. The right combination is the one that improves the operator’s task on the finished screen, not the one with the longest treatment name.
Related product information: Anti-Glare AG Glass, Anti-Reflective AR Glass and Industrial HMI Glass.